The tear test measures the force, or the energy, needed to start or propagate a tear in a standardized test specimen of rubber, plastic film, fabric or leather. For rubber, the result is the force divided by the thickness, in kN/m (equal to N/mm). For film and fabric, the result is the force itself, in N. You cannot compare results from different standards or geometries.
The standard depends on the material. For rubber, it is ASTM D624-00(2020) or ISO 34-1:2022. For film, it is ASTM D1938-19 (trouser) or ASTM D1004-21 (Graves). For fabric, it is ASTM D2261-13(2024), ASTM D5587-15(2024) or the ISO 13937 series. For leather, it is ISO 3377. This guide covers what tear testing measures, the formula and units, the test specimens, a table of standards with editions checked on 10/13/2026, the test for each material, the Elmendorf pendulum, a step-by-step procedure on the universal testing machine, worked examples and the most common mistakes.
What the tear test is and what it measures
Tearing is a failure that starts at a stress concentration (a cut, a notch or a sharp corner) and grows from there. The tear test measures how well the material resists that growth. It differs from the tensile test in where the failure starts. In tension, the whole cross-section carries the load and the result is a stress. In tearing, the force concentrates in a small region at the tip of the flaw, and the material fails there bit by bit, long before the whole section reaches its strength.
The test exists because many products fail this way in service. ASTM D624 notes that rubbers and thermoplastic elastomers often fail when tears form and grow. The same is true for a plastic bag that tears from a hole, a glove that splits from a small cut, a tarpaulin that tears from a grommet and leather upholstery that gives way at the seam. This is why tear testing is part of the development and quality control of seals, hoses, belts, footwear, gloves and catheters; of packaging films, trash bags and agricultural films; of workwear fabrics, airbags, tarpaulins and geotextiles; and of leather for footwear and upholstery.
The same standard adds a caveat that applies to the whole subject. The result is valid for the conditions of that test and may have no direct relation to how the product performs in service. The value depends on the specimen shape, the speed, the temperature and the orientation of the material. The test is for comparing materials and batches tested the same way. It does not give a design value.
Tear strength: what the term means
Tear strength (also called tear resistance) is the value the test gives: the force to start or propagate the tear, or that force divided by the thickness. The standards use both terms as synonyms: D624 says "tear strength", D1004 says "tear resistance" and D1938 says "tear-propagation resistance". Some texts use "tear strength" for propagation and "tear resistance" for initiation, but the standards make no such distinction. Initiation and propagation are separated by the specimen geometry, as the next section shows.
Tear initiation and tear propagation
A tear has two phases. In initiation, the intact material has to form the crack at the point of highest stress. In propagation, the crack already exists and grows. The standards pick a phase through the shape of the specimen:
- No prior cut, angled corner: the corner concentrates the stress and the tear starts there. ASTM D1004 (Graves, for film) measures the maximum force, which occurs near the start of the tear. For the unnicked 90° angle specimen used for rubber (D624 type C, ISO 34-1 method B), the official ISO 34-1 abstract says the measured force combines initiation and propagation, and the two parts cannot be separated.
- With a nick or cut made before the test: the crack is already there, and the test measures propagation. This applies to the nicked crescent, trouser, tongue and trapezoid specimens and to the Elmendorf pendulum.
The table summarizes what each geometry measures and where it is used:
| Measures | Geometry | Standards |
|---|---|---|
| Initiation and propagation, combined | unnicked 90° angle | ASTM D624 type C; ISO 34-1 method B |
| Initiation (maximum force near the start) | Graves, film | ASTM D1004 |
| Propagation from a nick | nicked crescent or angle | ASTM D624 types A and B; ISO 34-1 methods B and C |
| Propagation from a cut | trouser, tongue, trapezoid, wing | D624 type T, ISO 34-1 A, D1938, ISO 6383-1, D2261, D5587, ISO 13937-2 to -4, ISO 3377 |
| Propagation, by energy | Elmendorf pendulum | ASTM D1922, D1424; ISO 6383-2, ISO 13937-1 |
Tear strength formula and units
For rubber, tear strength is the force divided by the specimen thickness: Ts = F / d, in N/mm, which is the same as kN/m. Dividing by the thickness makes sense because, in a rubber sheet, the tearing force increases in proportion to the thickness that has to be torn. What changes from one geometry to another is which force goes into the calculation:
- Angle and crescent (D624 types A, B and C; ISO 34-1 methods B and C): F is the maximum force, the peak of the curve.
- Trouser (ISO 34-1 method A; D624 type T): F is the propagation force, which oscillates as the tear advances. According to ZwickRoell, ISO 34-1 uses the median of the peaks, and D624 uses the mean or the median for types T and CP. Using the highest peak overestimates the result.
- Film and fabric: the result is usually the force itself, in N, not divided by the thickness. D1938 reports the average propagation force; D1004, the maximum force; D2261, the average of the five highest peaks or the single peak, depending on the option stated in the report.
- Elmendorf pendulum: the instrument converts the energy lost by the pendulum into an average tearing force, read in mN or in gf (gram-force).
Dividing by the thickness is not automatic for film. ASTM D1922 (pendulum) states that tearing force and thickness are not linearly related, and that only results from films of the same thickness should be compared. ASTM D1004 allows the result to be expressed per unit thickness only where the correlation has been shown for the material. Data sheets that give "g/µm" or "N/mm" for film apply a normalization that is useful as an indication, not as a material property.
In the fracture mechanics of elastomers, tearing is also described by the tearing energy, the energy spent per unit area of new crack. For a trouser specimen whose legs barely stretch, it equals T = 2F / t, in J/m², where F is the propagation force and t the thickness. Rivlin and Thomas (Journal of Polymer Science, 1953) showed that cut growth in rubber follows this energy criterion, practically independent of the specimen shape, and measured 1 to 20 kJ/m² in natural rubber vulcanizates. It is the same concept as toughness, applied to a highly deformable material.
The most common units and conversions (Biopdi calculation, with 1 lbf = 4.44822 N and 1 in = 25.4 mm):
| Quantity | Formula | Unit | Where it is used |
|---|---|---|---|
| Tear strength (peak) | Ts = Fmax / d | kN/m = N/mm | D624 A, B, C; ISO 34-1 B and C |
| Tear strength (trouser) | Ts = Fmedian / d | kN/m = N/mm | ISO 34-1 A; D624 T |
| Tearing force | average, maximum or peak F | N (lbf, gf) | film and fabric |
| Tearing energy | T = 2F / t | J/m² or kJ/m² | fracture mechanics of elastomers |
| Conversions | 1 lbf/in = 0.1751 N/mm; 1 gf = 9.807 mN; 1 N/mm = 1 kN/m | US data sheets and pendulum |
Tear test specimens
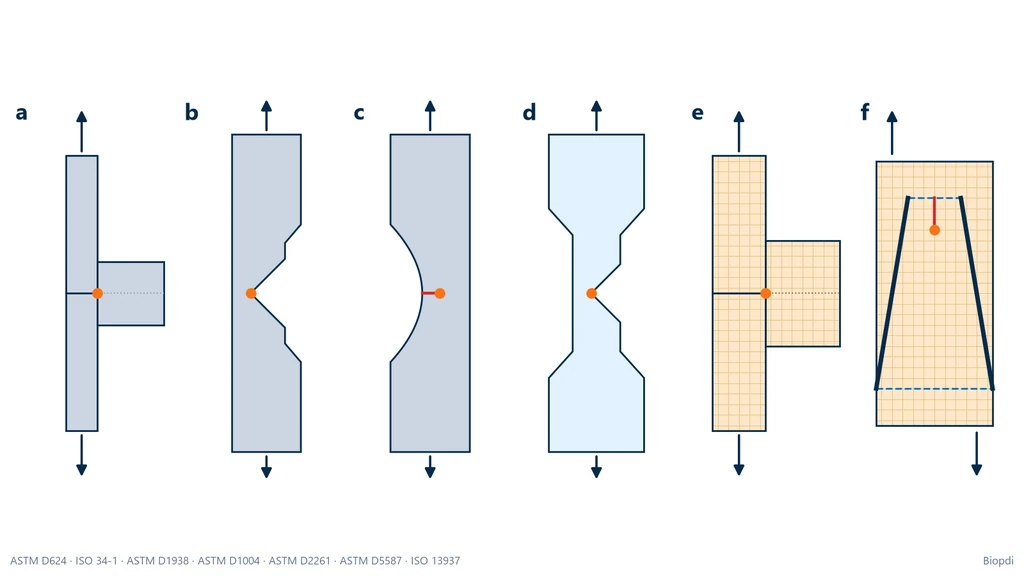
The test specimen defines the tear test: the same rubber gives different values in the trouser, angle and crescent specimens, because each shape concentrates the stress in a different way. This is why the standard specifies the shape, the dimensions, the cutting die or template and the depth of the nick. The diagram below shows, in plan view and without the dimensions from the standards, the six most widely used shapes. The trouser and tongue specimens are shown already opened in the test position, the others as they are before going into the grips. The cut is in red, the point where the tear starts or advances is in orange, and the arrows show the direction in which the grips move apart.
Trouser tear test
The trouser tear test uses a rectangular strip slit lengthwise down the middle, forming two "legs". Each leg goes into one grip, and the machine moves the grips apart at a constant speed so the tear propagates along the center line. Because the tear follows a set path, the force oscillates around a plateau, and the result is the median (or mean) of the peaks in that section. Of all the geometries, it comes closest to a pure measure of propagation, which is why it exists for almost every material: rubber (ISO 34-1 method A, ASTM D624 type T), film (ASTM D1938, ISO 6383-1), fabric (ISO 13937-2) and leather (ISO 3377-1, which ISO itself says is sometimes called the trouser tear). The speed varies between standards: 100 mm/min in ISO 34-1 and ISO 13937-2, 250 mm/min in D1938, 50 mm/min for D624 type T.
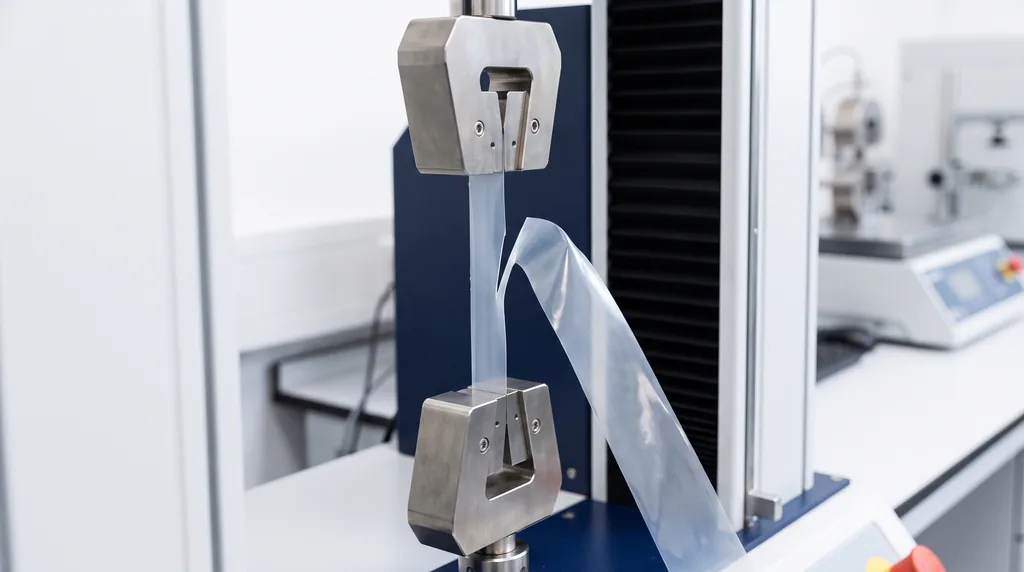
The photo shows a trouser tear test on plastic film. The strip has been slit lengthwise down the middle, one leg is clamped in the upper grip and the other in the lower grip, and the tear advances along the center line as the grips move apart. The still intact part of the film hangs between the grips, carrying no load.
The trouser specimen has one limitation: the legs stretch too. If the material is highly extensible, part of the force goes into stretching the legs rather than tearing. ISO 6383-1 warns that the method is not suitable for films in which leg deformation takes up a significant share of the energy. In those cases, another geometry is the right choice, such as the angle or crescent specimen.
Angle, crescent and Graves
The 90° angle specimen is a strip with a reentrant corner in the middle of one edge (D624 type C, the rubber geometry most often cited in US data sheets as "Die C"). Without a nick, the tear starts at the apex of the angle; with a nick, it starts from the nick. The crescent has a concave edge with a small nick at the center (D624 types A and B, ISO 34-1 method C) and measures the propagation of that nick. In both, the curve rises to a peak and drops as the tear crosses the width: the result is the maximum force divided by the thickness.
The Graves specimen is the film version of the 90° angle, defined by ASTM D1004-21: a specimen with wide tabs and a right angle at the center, pulled at 51 mm/min. The standard measures the force to initiate the tear (the maximum force occurs near the start), reports it in newtons and does not apply to films that fail in a brittle way or to materials that extend more than 101.6 mm before breaking. ASTM states that it knows of no equivalent ISO standard.
Tongue, trapezoid and wing (fabrics)
For fabric, the simple trouser strip has several variants. In the single tongue tear (ASTM D2261), a rectangle is slit down the middle from one of the short edges and each "tongue" goes into a grip, as in the trouser specimen, but with a wider specimen. In the double tongue tear (ISO 13937-4), two parallel cuts form a central tongue clamped in one grip, while the sides go into the other; the tear advances along both cuts. In the trapezoid (ASTM D5587), a trapezoid is marked on the rectangle, the two non-parallel sides are clamped in the grips and a short cut in the middle of the shorter base starts the tear, which advances across the width as the yarns are loaded one by one. In the wing specimen (ISO 13937-3), the ends are cut at an angle so that the tear follows the intended line.
Delft and Baumann: special specimens
Two names come up often in searches and data sheets. The Delft specimen is the small rubber specimen of ISO 34-2:2022, preferred when little material is available or when a small part is tested; ISO itself warns that it does not necessarily give the same result as ISO 34-1. The Baumann test is the double edge tear for leather, standardized by ISO 3377-2:2025, which ISO describes as "sometimes called Baumann tear". The single edge tear for leather, trouser type, is ISO 3377-1:2011.
Tear test standards by material
You choose the tear test standard by the material and by the stage of the tear you need to measure: rubber follows ASTM D624 or ISO 34-1; film, D1938, D1004 or ISO 6383; fabric, D2261, D5587 or ISO 13937; leather, ISO 3377. The table lists the main standards, with the edition and status checked in the ASTM store and the ISO catalog on 10/13/2026. Speeds marked with an asterisk come from equipment manufacturers and laboratories (ZwickRoell, Teartester, Universal Grip, Nelson Labs, MaterialsTests), not from the text of the standard. Check them against the purchased standard before you set up the test.
| Standard and edition | Material and specimen | Speed | Result |
|---|---|---|---|
| ASTM D624-00(2020), types A, B and C | rubber and TPE; nicked crescent (A, B), unnicked angle (C) | 500 ± 50 mm/min* | Fmax / thickness, kN/m |
| ASTM D624-00(2020), types T and CP | rubber and TPE; trouser (T) and CP | 50 ± 5 mm/min* | mean or median / thickness, kN/m |
| ISO 34-1:2022, method A | rubber; trouser | 100 ± 10 mm/min* | median / thickness, kN/m |
| ISO 34-1:2022, methods B and C | rubber; angle with or without nick, nicked crescent | 500 ± 50 mm/min* | Fmax / thickness, kN/m |
| ISO 34-2:2022 | rubber; Delft, small test pieces | as per the standard | force, as per the standard |
| ASTM D1938-19 | film and sheeting up to 1 mm; trouser, propagation | 250 mm/min* | average propagation force, N |
| ISO 6383-1:2015 | film and sheeting under 1 mm; trouser | as per the standard | propagation force, N |
| ASTM D1004-21 | film and sheeting; Graves, initiation | 51 mm/min | maximum force, N |
| ASTM D1922-23 and ISO 6383-2:1983 | film; Elmendorf pendulum | tear at 7.6 to 46 m/min (D1922) | mN or gf |
| ASTM D2261-13(2024) | fabric; tongue (single rip) | 300 mm/min* | average of the 5 highest peaks or single peak, N |
| ASTM D5587-15(2024) | fabric; trapezoid | 305 mm/min (12 in/min)* | tearing force, N |
| ISO 13937-2:2000 | fabric; trouser | 100 mm/min* | tearing force, N |
| ISO 13937-3:2000 and ISO 13937-4:2000 | fabric; wing (3) and double tongue (4) | as per the standard | tearing force, N |
| ASTM D1424-25 and ISO 13937-1:2000 | fabric; Elmendorf pendulum | pendulum | tearing force, N or mN |
| ISO 9073-4:2021 | nonwoven; trapezoid | as per the standard | tearing force, N |
| ISO 4674-1:2016 and ISO 4674-2:2021 | rubber- or plastics-coated fabric; tongue and trouser (1), pendulum (2) | constant (1); pendulum (2) | tearing force, N |
| ISO 3377-1:2011 and ISO 3377-2:2025 | leather; single edge (1) and double edge, Baumann (2) | as per the standard | tearing force, N |
On status: ISO 34-1:2022 and ISO 34-2:2022 replaced the 2015 editions, which have been withdrawn; all four parts of ISO 13937 were confirmed in 2023; ISO 3377-1:2011 is current but under revision; ISO 3377-2:2025 replaced the 2016 edition. At ASTM, D624 and D1938 remain at the 2000 edition (reapproved in 2020) and the 2019 edition, and D1424 got a new edition in 2025.
Brazilian standards. ABNT NBR 11911 (the Brazilian standard for tear strength of vulcanized elastomers) is listed as canceled without replacement since December 2013 in the Target catalog; anyone in Brazil who needs a method for rubber now uses ASTM D624 or ISO 34-1. There are Brazilian adoptions of the ISO 13937 series (such as ABNT NBR ISO 13937-2) and of ISO 3377, and ABNT NBR 8516 covers tear testing of flexible polyurethane foam; the current edition and status of these standards were not confirmed in the ABNT catalog as of the date of this article.
Rubber tear testing: ASTM D624 and ISO 34-1
Tear testing of rubber and thermoplastic elastomers follows ASTM D624-00(2020) or ISO 34-1:2022, and the result is given in kN/m, the force divided by the thickness. Both standards cover the same specimen families (trouser, angle and crescent), but with their own dimensions, speeds and calculation rules. ZwickRoell notes that D624 and ISO 34 results are not directly reproducible from one to the other: a "Die C" value on an American data sheet cannot be compared with an ISO trouser value on another data sheet.
In D624, types A and B are nicked crescents, type C is the unnicked 90° angle, type T is the trouser and type CP is another propagation specimen. According to ZwickRoell, types A, B and C run at 500 ± 50 mm/min and the result is the maximum force per thickness; types T and CP run at 50 ± 5 mm/min and the result is the mean or median propagation force per thickness. In ISO 34-1, method A (trouser, at 100 ± 10 mm/min) uses the median; methods B (angle, with or without nick) and C (nicked crescent), at 500 ± 50 mm/min, use the maximum force.
D624 points out that the result is strongly affected by the anisotropy that processing creates in rubber (the calendering or extrusion "grain"), by the strain rate and by the specimen size. In practice: always cut specimens in the same direction relative to the grain, or in both directions and report both; measure the thickness in the tear region; and nick with the specified tool, because a dull or overly deep nick changes the value. Temperature matters even more in rubber than in plastics: at high rates or low temperatures, the tearing energy can be 10 to 100 times higher (Polymer, 2013), which explains why some standards and specifications call for hot tear testing.
Anyone who tear tests rubber almost always also tensile tests the same compound, to ASTM D412 or ISO 37. These are different standards and specimens, run on the same machine; the guide to ASTM D412 and ISO 37 (rubber tensile testing) covers the second test.
Plastic film tear testing: ASTM D1938, D1004 and ISO 6383
For plastic film, ASTM D1938-19 (trouser) measures the force to propagate a tear and ASTM D1004-21 (Graves) measures the force to initiate it; both report the force in newtons. D1938 applies to film and sheeting up to 1 mm thick (ASTM calls material up to 0.25 mm film) and states that it is similar to ISO 6383-1 but not equivalent, because ISO uses a larger specimen and different speeds. D1004 states that the method is intended to rank materials of similar composition, not to predict the behavior of different products.
Film has a particularity that changes everything: anisotropy. During extrusion, the polymer chains orient in the machine direction (MD); in the transverse direction (TD), orientation is lower. A tear running parallel to the oriented chains meets less resistance, which is why film tears more easily in the MD. A bag that tears straight when opened one way and resists the other way is showing exactly this.
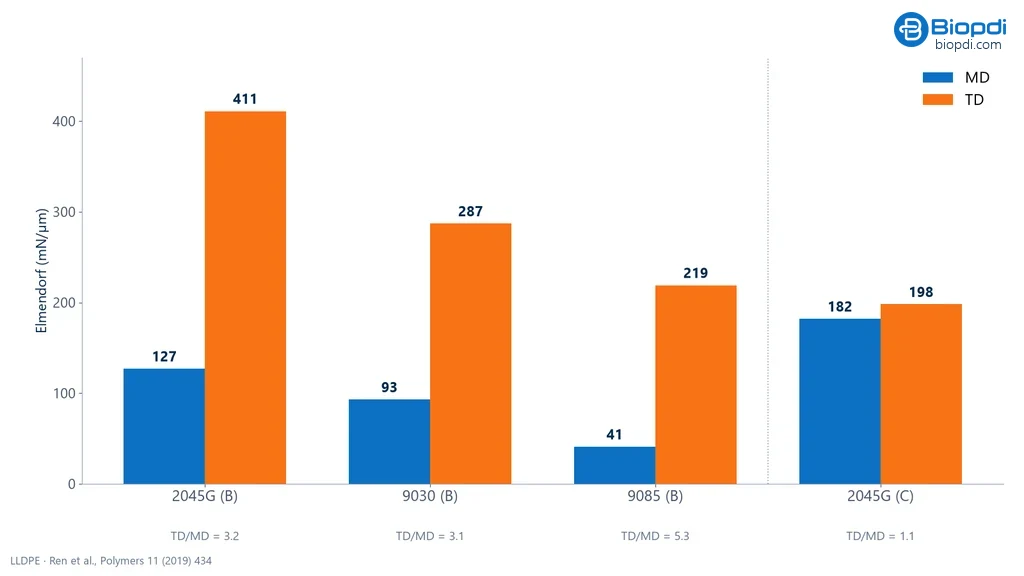
The chart below compares the Elmendorf tear resistance, in mN per µm of thickness, of three blown LLDPE films with different comonomers and one cast film, in both directions (Ren et al., Polymers, 2019). In the blown films, the TD was 3.1 to 5.3 times more tear resistant than the MD; in the cast film, where the chains are barely oriented, the two directions were close.
The consequence for the lab is straightforward: test film in both directions and report each separately. An average of the two hides the weak point, which is the MD. The same goes for thickness: compare films of the same thickness, because the relationship between tearing force and thickness is not linear. Tensile testing of the same film follows ASTM D882, covered in the guide to ASTM D882 (tensile testing of plastic films). There is also a test that combines puncture and tear, ASTM D2582, used for films that tear from a sharp object.
Fabric and leather tear testing: ASTM D2261, D5587, ISO 13937 and ISO 3377
For fabric, tear strength is measured by the single-rip tongue (ASTM D2261), the trapezoid (ASTM D5587), the four parts of ISO 13937 or the pendulum (ASTM D1424), and the result is the tearing force in newtons, reported separately for warp and weft. D2261 and D5587 state that the constant-rate-of-extension (CRE) machine is the preferred apparatus; in D5587, the result obtained on the CRE machine prevails over that of the constant-rate-of-traverse (CRT) machine, which is used only by agreement between the parties. The CRE machine is the electromechanical universal testing machine.
In fabric, the tear advances yarn by yarn. Each time a group of yarns at the tear front breaks, the force drops; then it rises until the next group breaks. The curve is a series of irregular peaks. D2261 notes that the highest peaks reflect the strength of the yarns that stop the tear and that the valleys have no significance; that is why the calculation uses the peaks. According to Universal Grip, D2261 uses a 75 × 200 mm specimen, a 75 mm cut, 300 mm/min and the average of the five highest peaks; the standard's other option is the single peak. For ISO 13937-2 (trouser), according to MaterialsTests, the specimen is 200 × 50 mm, with a 100 mm cut, a speed of 100 mm/min and at least five specimens per direction.
Fabric construction determines the result. In a study of plain and rib (rep) weaves, tear strength in the weft was much higher than in the warp because the warp yarn density (65 yarns/cm) was much higher than the weft density (14 to 20 yarns/cm); filament yarns gave the highest tear strength, and high density reduced tear strength (Eryuruk and Kalaoglu, AUTEX Research Journal, 2015). The reason is mobility: in an open fabric, the yarns at the tear front slide and bunch together, sharing the load; in a dense fabric, they are locked in place and break one by one. The standard for nonwovens is ISO 9073-4:2021 (trapezoid), and for rubber- or plastics-coated fabric, ISO 4674-1:2016 (tongue and trouser) and ISO 4674-2:2021 (pendulum). Tarpaulins, awnings and geotextiles follow the same reasoning, with their own product standards.
For leather, ISO 3377-1:2011 (single edge, trouser type) and ISO 3377-2:2025 (double edge, Baumann) measure the force to tear from a cut. As with fabric, the cut direction matters, and the report states where and in which direction each specimen was taken.
Elmendorf pendulum: an energy-based method
The Elmendorf test measures tear propagation resistance from the energy a pendulum loses while tearing the specimen; the result is an average force, in mN or gf, and it does not convert into a trouser tear result. The specimen is held between a fixed clamp and a clamp attached to the pendulum; a knife makes the initial cut, the pendulum is released, swings down and tears the rest. The instrument converts the energy lost into an average tearing force. The standards are ASTM D1922-23 and ISO 6383-2:1983 for film, ASTM D1424-25 and ISO 13937-1:2000 for fabric, ISO 4674-2:2021 for coated fabric and TAPPI T414 for paper, where several sheets are torn together.
Three differences set the pendulum apart from the universal testing machine. Speed: in D1922, the tear runs at 7.6 to 46 m/min, 30 to almost 200 times faster than the D1938 trouser test at 250 mm/min. Principle: the pendulum measures the energy spent over a short path, with no force curve. Equipment: it is a dedicated instrument that cannot be mounted on a universal testing machine. That is why the ISO 4674-2 abstract warns that pendulum results are not comparable with constant-speed methods, and D1424 is only valid if the fabric tears in the intended direction, without deviating.
The pendulum dominates commercial "tear tester" pages because it is fast and is the historical reference for film and paper. The universal testing machine is the choice for force-based methods (trouser, angle, crescent, Graves, tongue and trapezoid), which are the rubber methods and the ones ASTM prefers for fabric. The choice follows the customer's specification: if it calls for Elmendorf, the test is done on the pendulum; if it calls for trouser, Graves, tongue or trapezoid, it is done on the universal testing machine.
How to perform a tear test on a universal testing machine
On a universal testing machine, a tear test consists of clamping the test specimen between two grips, separating them at constant speed and recording the force-displacement curve until the tear runs through the specimen. Each standard adds its own details to this general procedure:
- Condition. Rubber, film and fabric each have their own temperature and humidity conditions, set in the test standard or in the conditioning standard it cites. Fabric is sensitive to humidity; rubber, to temperature.
- Cut specimens in both directions (MD and TD for film; warp and weft for fabric; with and across the grain for rubber), using a sharp die or template. Jagged edges create tear initiation points in the wrong place.
- Make the cut or notch at the position and depth set by the standard, with the specified tool. This is the step that causes the most scatter in results.
- Measure the thickness in the region the tear will pass through. For rubber, D624 uses the median of the readings.
- Clamp the specimen with no slack and no slippage. For trouser and tongue specimens, one leg in each grip; for trapezoid, the non-parallel sides in the grips; for angle and crescent, the tabs.
- Set the speed required by the standard and zero the force with the specimen mounted but unloaded.
- Record the whole curve, up to complete separation or the end of the measurement section.
- Discard any specimen in which the tear deviated from the intended line or ran out through the side, or that slipped in the grip, and test another one.
- Calculate and report: standard and edition, specimen type, direction, thickness, speed, temperature, individual values, median or mean, scatter and any tear deviation.
The test does not use an extensometer: what matters is the force, and the displacement is that of the crosshead. Nor is there a stress-strain curve, because the resisting area changes at every instant.
How to read the force-displacement curve
The shape of the curve tells you which force goes into the calculation. The diagram below uses the numbers from the worked examples in this article to show the three patterns: in (a), the unnicked angle specimen rises to a single peak of 85.0 N and drops when the tear runs through; in (b), the trouser specimen rises, reaches a plateau and oscillates in seven peaks, whose dashed median is 18.1 N; in (c), the fabric in the tongue test forms irregular peaks, and the five highest, in dark blue, give a mean of 41.6 N.
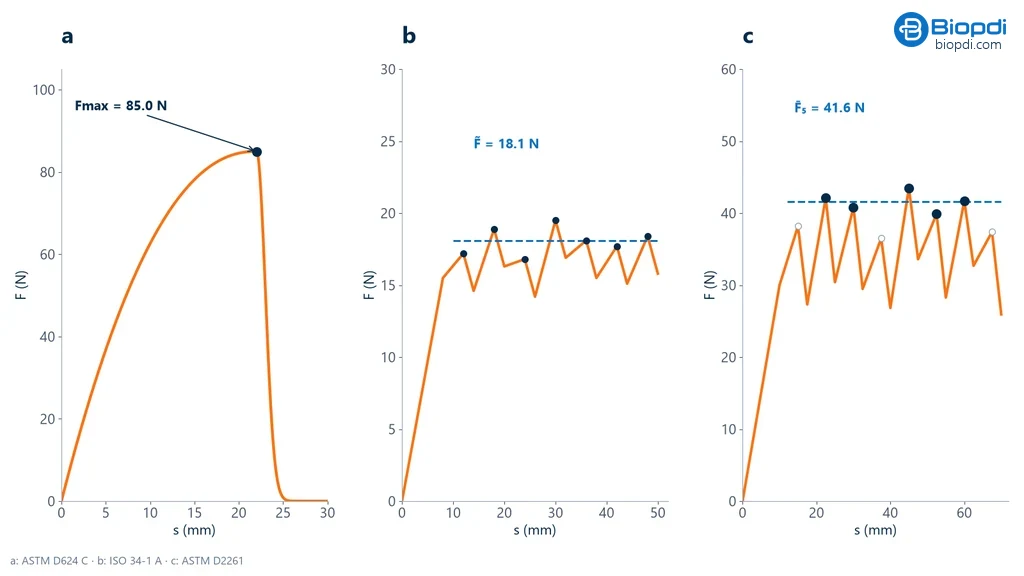
The oscillation of the trouser curve has a physical cause: the tear advances in jumps. The crack tip stores energy, advances all at once, the force drops and then rises again (the phenomenon called stick-slip, described in elastomers by Shrimali and Lopez-Pamies, 2023). That is why the standards use the median or the mean of the peaks, not the highest one. The initial section, in which the legs align and the tear has not yet started to run, is left out of the calculation. A sudden drop to zero in the middle of the plateau is usually slippage in the grip, not tearing.
Worked examples of tear strength
The examples below are illustrative, with numbers consistent with published ranges, and the calculations are Biopdi's. Examples 1 and 2 are different compounds and different geometries: they cannot be compared with each other.
1. Rubber, ASTM D624 type C (angle, peak). An EPDM specimen with a median thickness of 2.10 mm broke at a maximum force of 85.0 N at 500 mm/min. Ts = 85.0 / 2.10 = 40.5 N/mm = 40.5 kN/m. In US units: 40.5 / 0.1751 = 231 lbf/in. The value applies to type C; the same compound would give a different number with the crescent or trouser specimen.
2. Rubber, ISO 34-1 method A (trouser, median). Thickness 2.00 mm, 100 mm/min. Peaks in the propagation section: 17.2; 18.9; 16.8; 19.5; 18.1; 17.7; 18.4 N. In order: 16.8; 17.2; 17.7; 18.1; 18.4; 18.9; 19.5. The median is the fourth value, 18.1 N (the mean would be 18.09 N). Ts = 18.1 / 2.00 = 9.05 kN/m. The tearing energy, with legs of low extensibility, is T = 2 × 18.1 / 0.00200 = 18,100 J/m² = 18.1 kJ/m², within the 1 to 20 kJ/m² range measured by Rivlin and Thomas in natural rubber. Had the laboratory used the highest peak (19.5 N), it would have reported 9.75 kN/m, 8% higher.
3. Film, trouser and Elmendorf. (a) A 50 µm PE film gave an average propagation force of 0.42 N under ASTM D1938, at 250 mm/min. The result reported is 0.42 N, together with the thickness. Dividing by 0.050 mm (8.4 N/mm) only makes sense with a correlation demonstrated for the material. (b) An LDPE data sheet (Tricon, 2021) gives an Elmendorf value of 340 g at 50.8 µm. In SI: 340 × 9.807 = 3,334 mN = 3.33 N, or 65.6 mN/µm. This value cannot be compared with the 0.42 N from the trouser test: the methods and speeds are different. (c) In the data of Ren et al. (2019), blown LLDPE 2045G has TD/MD = 411 / 127 = 3.2: the film resists tearing three times more in one direction than in the other.
4. Fabric, ASTM D2261 (tongue). Peaks in the warp direction: 38.2; 42.1; 40.8; 36.5; 43.5; 39.9; 41.7; 37.4 N. The five highest are 43.5; 42.1; 41.7; 40.8 and 39.9, which add up to 208.0 N: a mean of 41.6 N. With the single-peak option, the result would be 43.5 N. If the weft gave 58.3 N, the weft/warp ratio is 58.3 / 41.6 = 1.40. The report gives both directions and states which calculation option was used.
5. Converting a US data sheet. A silicone data sheet states "Tear, Die B: 187 lbf/in". In SI: 187 × 0.1751 = 32.7 kN/m. The conversion changes the unit, not the method: the value is still from the D624 type B crescent specimen and cannot be compared with an ISO trouser test.
Tear strength and tensile strength
Tensile strength measures the stress an intact cross-section can withstand, in MPa; tear strength measures the force needed to make a flaw advance, in N/mm or N, and the two properties do not go hand in hand. In tension, the load is distributed over the whole cross-section up to the ultimate tensile strength; in tearing, it concentrates at the tip of the cut, and what matters is the material's ability to deform and dissipate energy in that region. That is why the units are different (N/mm² for tension, N/mm for tearing) and cannot be converted into each other.
A material can be strong in tension and weak in tearing. In fabric, increasing the thread density increases tensile strength, because more threads carry the load, but reduces tear strength, because the constrained threads cannot bunch together ahead of the crack (Eryuruk and Kalaoglu, 2015). In oriented film, the direction with the highest tensile strength is often the one that tears most easily. In rubber, reinforcing fillers and the type of vulcanization change tensile and tear strength in different proportions.
The equipment is the same; the standards are not. Some texts on the internet state that rubber tear strength "is measured by ASTM D412". It is not: ASTM D412 and ISO 37 are the rubber tensile test standards; rubber tear testing follows ASTM D624 or ISO 34-1. What the two families share is the universal testing machine, the load cell and the grips.
Common mistakes in tear testing
The mistakes that most distort the result, or how it is read:
- Citing ASTM D412 as a tear standard. It is a tensile standard; rubber tear testing is D624 or ISO 34-1.
- Comparing different geometries or standards. Trouser, angle and crescent specimens give different values on the same material, and D624 and ISO 34 are not directly reproducible with each other.
- Comparing Elmendorf with trouser tear. The principles and speeds are different.
- Using the highest peak in the trouser test instead of the median or mean of the propagation section.
- Dividing film force by thickness without a demonstrated correlation, or comparing films of different thicknesses.
- Testing only one direction. MD and TD, or warp and weft, can differ by more than a factor of three.
- Poorly made notch, with a dull blade or the wrong depth.
- Accepting a deviated tear or one that ran out through the side: the specimen must be discarded.
- Mistaking grip slippage for a tear peak.
- Ignoring speed and temperature, which change the result considerably in rubber.
- Using a withdrawn edition, such as ISO 34-1:2015 or ISO 3377-2:2016.
- Reading the result as a design value. D624 warns that it may have no direct relation to service performance.
- Confusing terms. On its own, "tear test" also refers to the Schirmer test of tear production in ophthalmology; "wear and tear" means wear; the "dynamic tear test" (ASTM E604) is a fracture test for metals, in the family of the impact test; bursting and puncture are different tests.
Tear testing on the Biopdi universal testing machine
Force-based tear methods (trouser, angle, crescent, Graves, tongue and trapezoid) are performed on a constant-speed universal testing machine, with a load cell sized for a few newtons up to a few hundred newtons and tensile grips. The Biopdi universal testing machine lists tear testing among its tests, and the BioLab software has a tear test configuration that calculates the maximum force and the tear strength in N/mm. Biopdi does not manufacture an Elmendorf pendulum. The panel below shows the machine, the role of each part in the tear test and the grips that hold the legs and tabs of the specimen.
The universal testing machine in the tear test
The M2 line has single-column models, from 200 N to 10 kN, and dual-column models, from 5 kN to 1,000 kN. Each part of the machine has a function in the test:
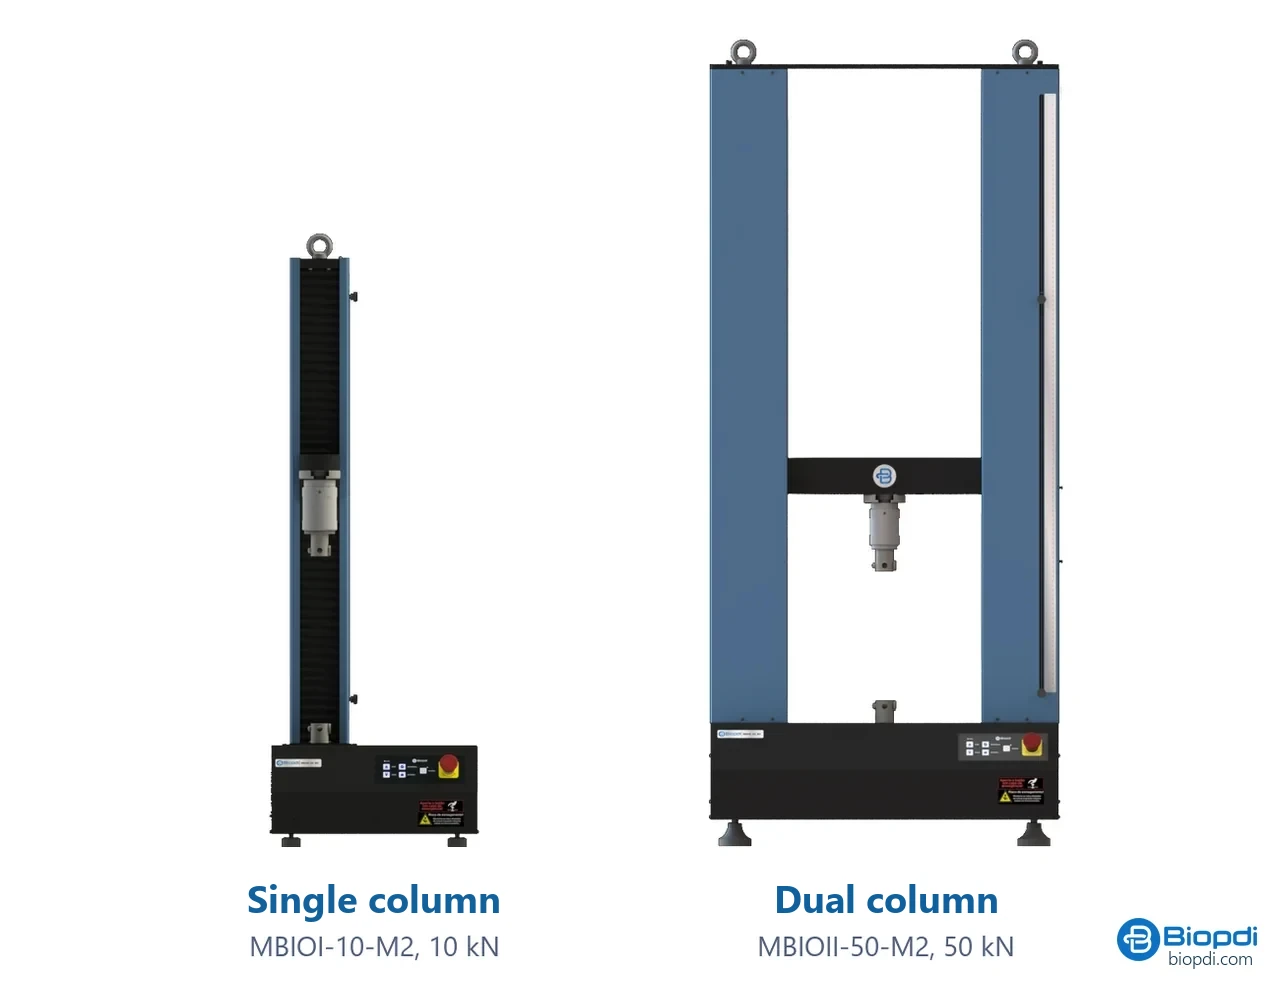
- Moving crosshead separates the grips at the speed set by the standard
- Load cell small, for forces of a few newtons
- Grips one leg or tab in each grip, without slipping
- Displacement from the crosshead, no extensometer
- BioLab software maximum force and tear strength in N/mm
- Control panel and emergency stop positions and stops the test
Fixtures for tear testing
The grips below are mounted on the same machine, depending on the material and the specimen:
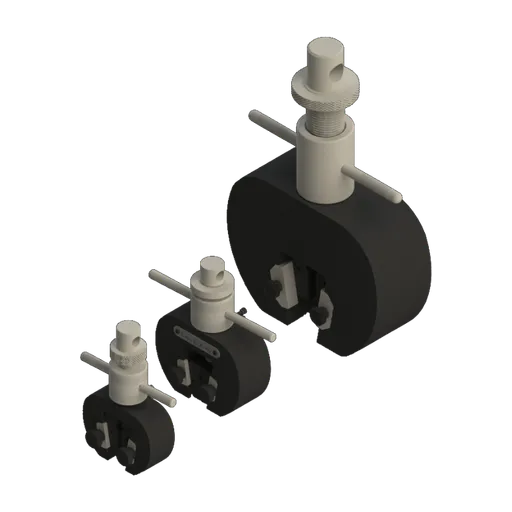
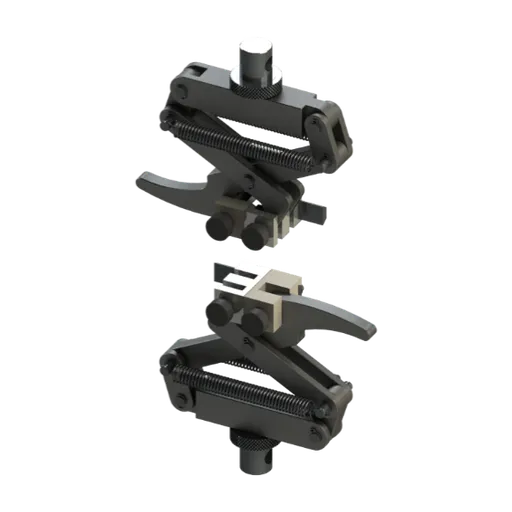
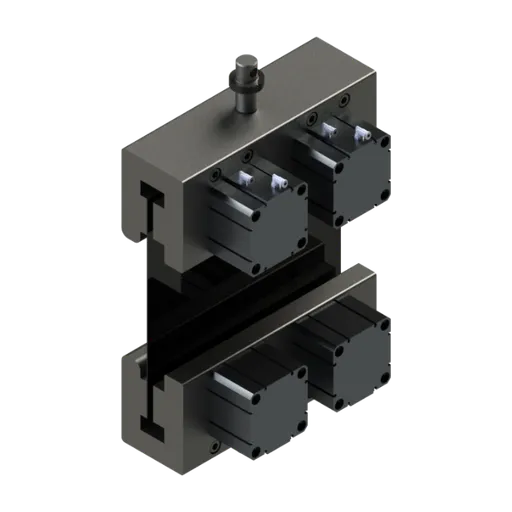
The selection rule is to size the load cell to the expected force. Film tearing gives from fractions of a newton to a few newtons; rubber and fabric, from tens to a few hundred newtons. The line has load cells starting at 0.05 kN, and the capacities suited to tear testing are the smallest ones. As for speed, D624 requires 500 ± 50 mm/min for types A, B and C: the models in the table reach 500 mm/min (the portable one, 600 mm/min), which meets that speed, and the other tear standards call for lower speeds. The extended column is for rubber trouser tests, whose legs stretch a great deal before the tear starts to run. To compare models and configurations, see how to choose a universal testing machine.
| Application | Range | Biopdi model |
|---|---|---|
| Films, paper, tapes | 200 N to 1 kN; 0.01 to 600 mm/min | MBIOI-1P-M2 portable |
| Rubber, films, fabrics | 2 to 10 kN; 0.01 to 500 mm/min | MBIOI-10-M2 |
| High-elongation rubber and films, stretch fabrics | 2 to 10 kN; 1,290 mm stroke | MBIOI-10-M2 extended column |
Tear testing is one of the mechanical tests the same universal testing machine performs; an overview of how the mechanical properties of materials relate to each other helps decide which tests to request alongside it.
Other tests and technical references
Tests performed on the Biopdi universal testing machine
Related technical references
Peel test: 90°, 180°, T-peel and peel strength calculation
The peel test measures the force per unit width needed to separate bonded materials. See 90°, 180° and T-peel, formula, units and ASTM and ISO standards.
ASTM D695: compression testing of rigid plastics (test specimen, 1.3 mm/min and calculations)
ASTM D695-26 measures compressive strength, yield and modulus of rigid plastics: a 12.7 × 12.7 × 25.4 mm prism at 1.3 mm/min. Calculations and ISO 604.
Puncture resistance test: standards, methods and calculation
Puncture resistance test: the force and energy for a probe to pierce films, geomembranes, geotextiles and gloves. ASTM, ISO, EN standards and calculation.
Frequently asked questions
What is a tear test?
A tear test measures the force, or the energy, needed to start or propagate a tear in a standard test specimen of rubber, plastic film, fabric or leather. For rubber, the result is force per thickness in kN/m (ASTM D624, ISO 34-1:2022). For film and fabric, it is the force in N.
What is the formula for tear strength?
Ts = F / d, the force divided by the thickness. For the angle and crescent specimens, F is the maximum force. For the trouser specimen, F is the median (or the mean) of the propagation peaks. Example: 85.0 N / 2.10 mm = 40.5 kN/m.
What is the unit of tear strength?
For rubber, N/mm, which equals kN/m. In the United States, lbf/in is used (1 lbf/in = 0.1751 N/mm). Film and fabric results are usually reported as force only, in N, and the Elmendorf pendulum reports in mN or gf (1 gf = 9.807 mN).
What is the ASTM standard for tear strength?
It depends on the material. For rubber, ASTM D624. For film, D1938 (trouser), D1004 (Graves) and D1922 (pendulum). For fabric, D2261 (tongue), D5587 (trapezoid) and D1424 (pendulum). As of October 13, 2026, the current editions are D624-00(2020), D1938-19, D1004-21, D1922-23, D2261-13(2024), D5587-15(2024) and D1424-25.
What is the trouser tear test?
In this test, a strip is slit lengthwise down the middle to form two legs, and each leg is clamped in a grip. The machine pulls the grips apart at constant speed and measures the force needed to propagate the tear. Because this force fluctuates, the result is the median of the peaks. Trouser tear methods exist for rubber (ISO 34-1, D624 type T), film (D1938, ISO 6383-1), fabric (ISO 13937-2) and leather (ISO 3377-1).
What is the difference between tear strength and tensile strength?
Tensile strength is the stress an intact cross-section can withstand, in MPa. Tear strength is the force needed to advance a cut or notch, in N/mm or N. The two do not necessarily go together: in fabric, a higher yarn density raises tensile strength but lowers tear strength. The standards are different too: the rubber tensile test is ASTM D412 or ISO 37, while the tear test is D624 or ISO 34-1.
What are the Graves tear and tongue tear tests?
The Graves tear test is ASTM D1004-21. A film specimen with a 90° angle at its center is pulled at 51 mm/min to measure the force needed to initiate the tear. The tongue tear test is a fabric test. In ASTM D2261 (single tear), the specimen is slit down the middle and each tongue is clamped in its own grip. In ISO 13937-4 (double tear), the central tongue goes in one grip and the two side tongues go in the other.
What is the Baumann tear test?
It is a double edge tear test for leather, standardized in ISO 3377-2:2025. ISO notes that this method is sometimes called the Baumann tear. The single edge (trouser) tear test for leather is ISO 3377-1:2011.
Which machine measures tear strength?
The force-based methods (trouser, angle, crescent, Graves, tongue and trapezoid) use a constant-rate-of-extension (CRE) universal testing machine with a low-capacity load cell and tensile grips. ASTM D2261 and D5587 name the CRE machine as the preferred apparatus. The energy-based methods use the Elmendorf pendulum, a different instrument, and its results cannot be converted into those of a universal testing machine.
Which fabric is the most tear resistant?
No single fabric is. Tear strength is higher in fabrics with strong, mobile yarns, such as filament yarns, which bunch together ahead of the tear and share the load. It is also higher in constructions with anti-tear reinforcement (ripstop). Very dense fabrics tend to tear more easily, because yarns that cannot move break one at a time (Eryuruk and Kalaoglu, 2015).
Why test film and fabric in both directions?
Because they are anisotropic. In one blown LLDPE film, the Elmendorf tear strength was 127 mN/µm in the machine direction and 411 mN/µm in the transverse direction (Ren et al., 2019). In fabric, warp and weft also give different results. Reporting only one direction hides the weak one.