The bend test is a qualitative test in which a test specimen is bent over a mandrel (former or pin) of defined diameter to a specified angle, usually 90° or 180°. The result is pass or fail, depending on whether cracks appear on the tension face. It evaluates the ductility and soundness of the material and, above all, of welded joints and rebar. The general standards are ISO 7438 (ABNT NBR ISO 7438 in Brazil) and ASTM E290. For welds, they are ISO 5173, ASME IX and AWS D1.1. For rebar, they are NBR 7480 (the Brazilian standard for steel reinforcing bars) and NBR 17005 (the Brazilian bend test method for reinforcing bars).
The bend test does not measure strength in MPa: that is the job of the flexural test. It answers a more direct, shop-floor question: can this material, or this weld, be bent without cracking? In this guide you will find the types of bend test, the strain imposed by the mandrel, the test specimen, the procedure, the mandrels for Brazilian CA-25, CA-50 and CA-60 rebar, weld bend testing and its acceptance criteria, worked examples, the standards and the most common mistakes.
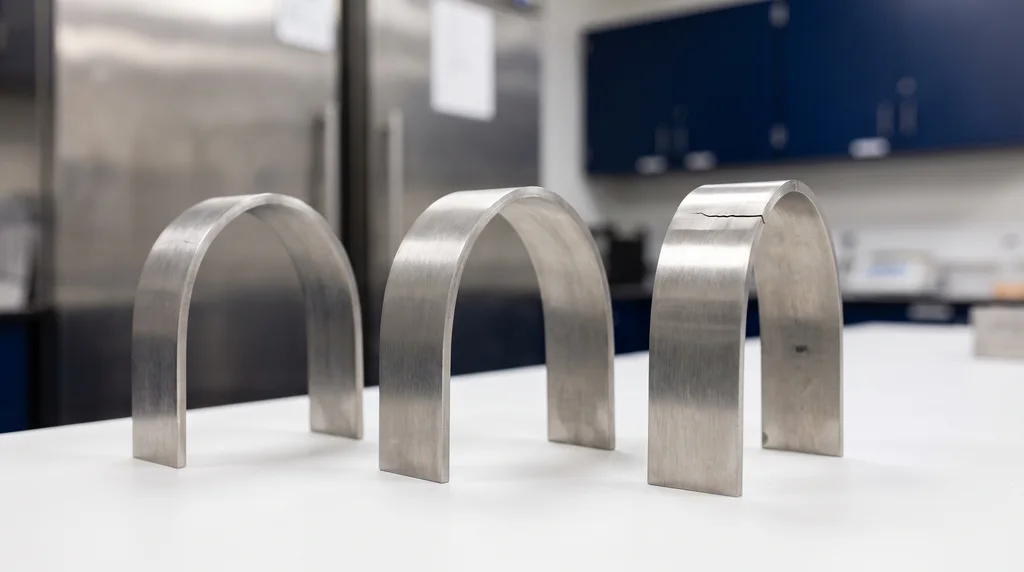
The photo shows the result of a test: three steel specimens bent to 180°. The two on the left reached the angle without cracking; the one on the right opened a crack at the top of the outer face, the tension face, and failed.
What is the bend test
ASTM E290-22 defines the test as a bend test "for ductility" of the material: after bending, the convex surface (the outside of the bend) is examined; if the specimen fractures, the material has failed; if it does not fracture, the criterion is the number and size of cracks visible to the unaided eye, as set by the product specification. ISO 7438:2020 describes the principle: the specimen, with a round, square, rectangular or polygonal cross section, is plastically deformed by bending, without reversing the direction of loading, until the specified angle is reached. At 180°, the legs may be in contact or parallel at a distance controlled by a spacer.
In the bend, the outer face is in tension and the inner face in compression. A ductile material accommodates this deformation; a brittle material, a weld with lack of fusion or a bar with a surface defect opens cracks on the outer face. The underlying property is ductility: the ability to deform plastically without fracturing.
The most common setup is the guided bend, and the three diagrams below show the setup, the bend and how the angle is measured. In the first, the specimen, with a round or rectangular cross section, rests on two supports, with the mandrel of diameter D in the middle. In the second, the force Q has already bent the specimen around the mandrel, and the outside of the bend, the tension zone, is the face to be examined. The third shows the bend angle α, which is how far the leg has rotated relative to the original axis of the specimen: at 180°, the two legs are parallel.
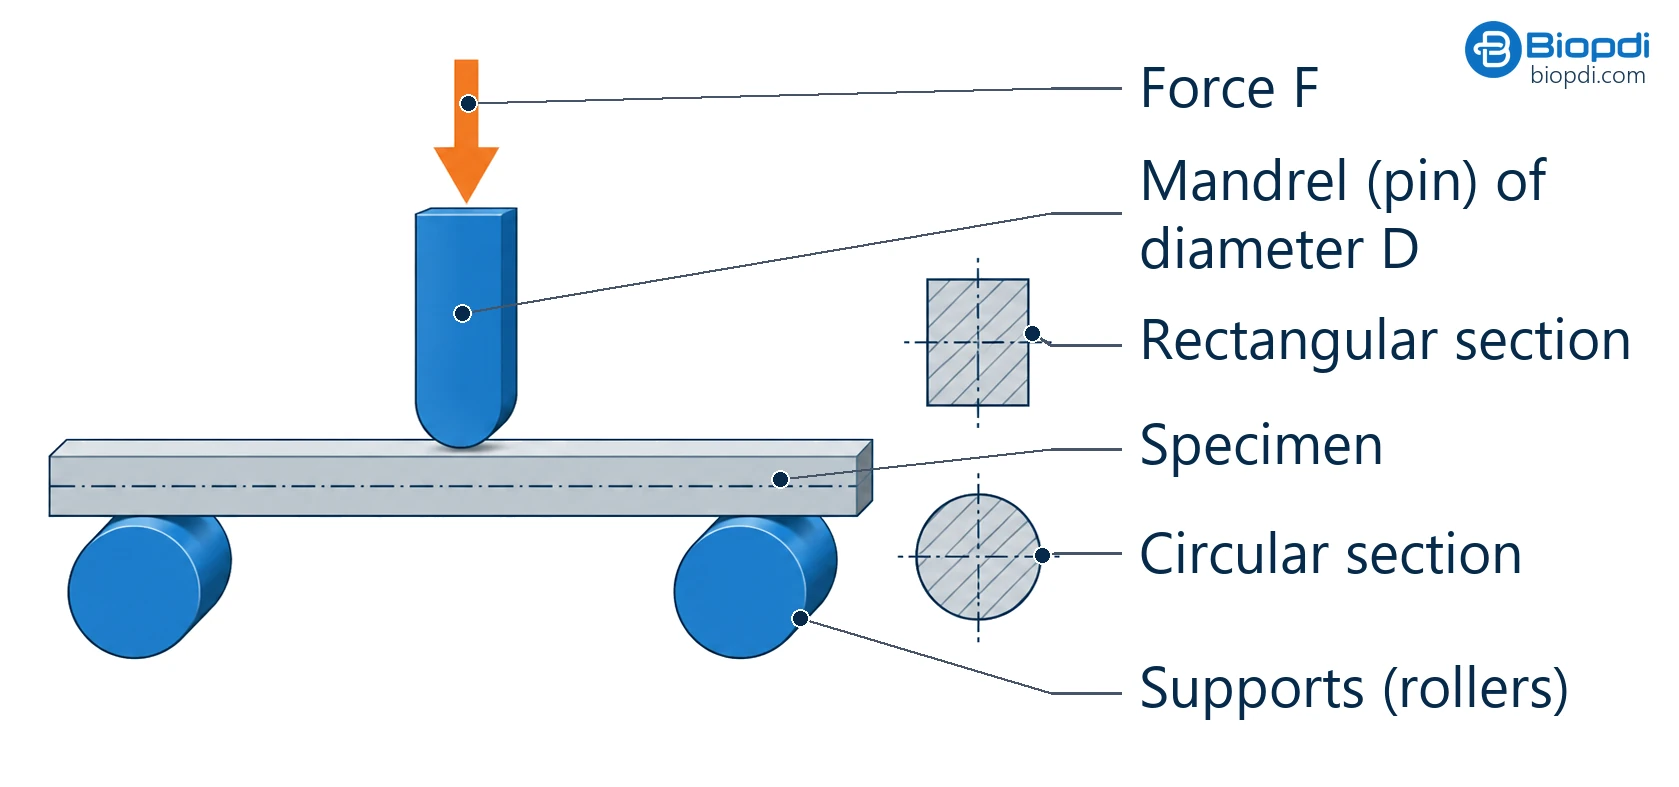
Guided bend: two supports and a mandrel (pin) of diameter D
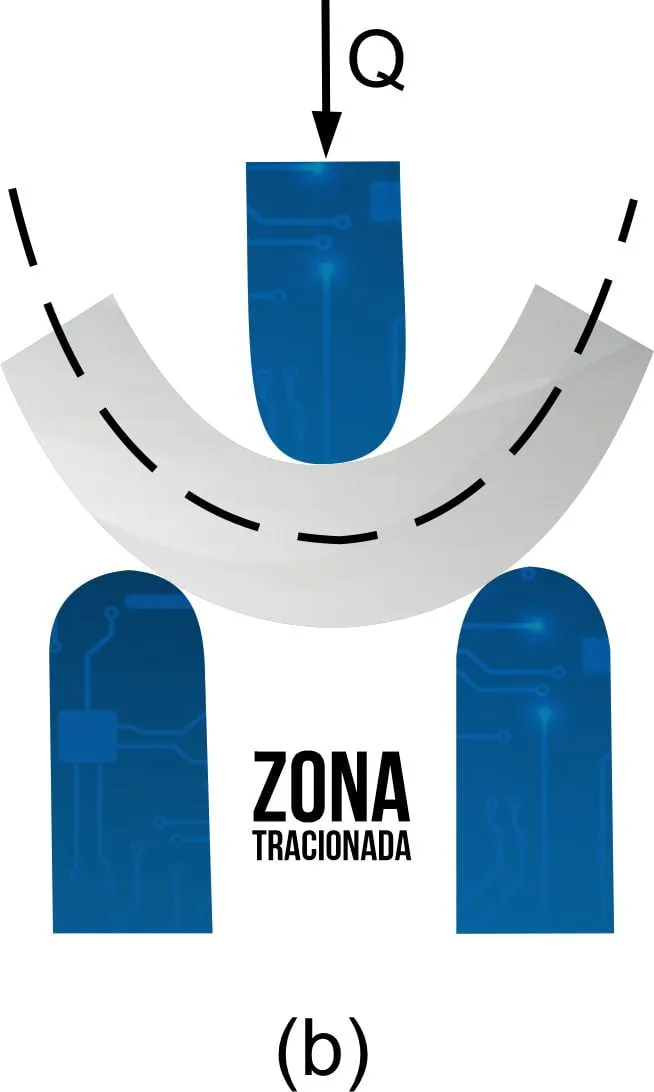
Guided bend: the outer face is in tension
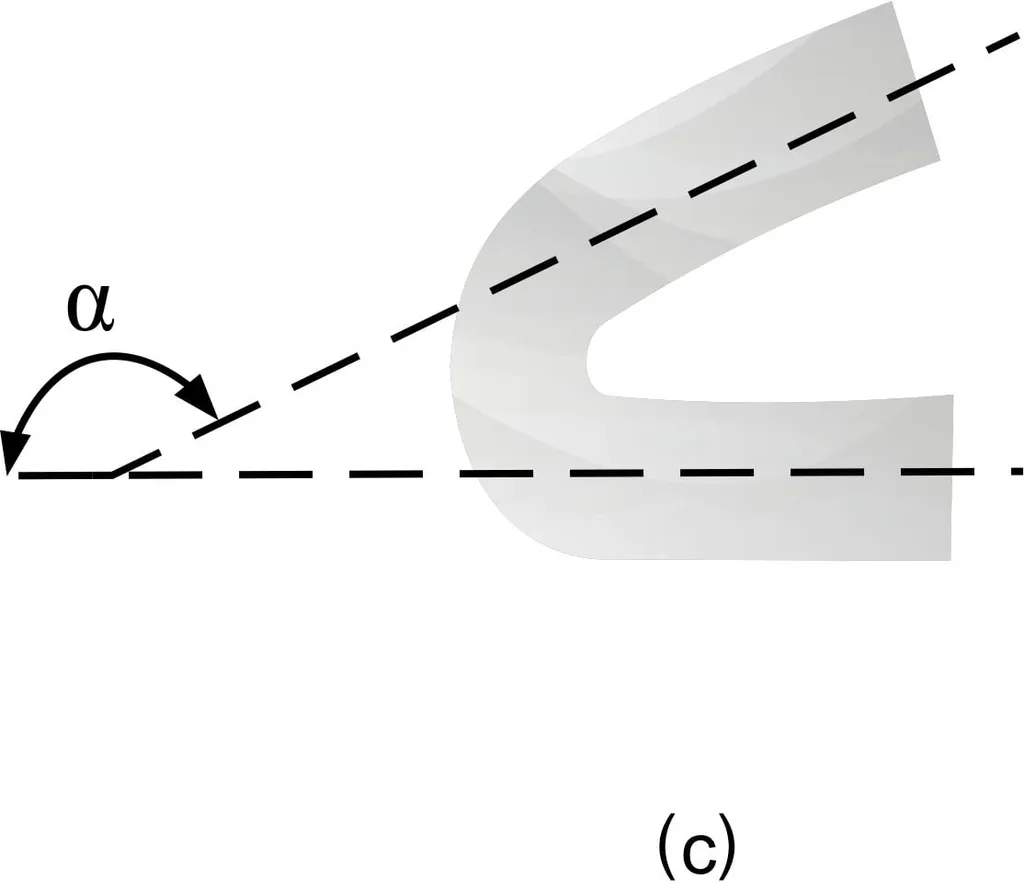
Bend angle (α)
What it is used for and what its limits are
The test is so widely used in welder qualification and in the release of rebar lots because it is simple, fast and inexpensive: the fixture is a pair of supports and a mandrel, and the result comes from a visual inspection. At the same time, it is severe where it matters. The bend concentrates the deformation in a small region and takes it far beyond what the part experiences in service, so it reveals lack of fusion, slag inclusions, porosity and surface defects that a tensile test may not show. A lot that starts failing the bend test points to a process deviation: welding parameters, rolling, heat treatment or raw material.
The limit is the other side of the same simplicity: the test does not give a design number. It does not measure yield strength, tensile strength, impact toughness or fatigue strength, and the result is valid only for the mandrel, angle and preparation used. That is why it complements the tensile test without replacing it: in rebar release and in welding procedure qualification, both are required together.
Types of bend test
The types differ in how much the tooling controls the shape of the bend. ASTM E290 defines four conditions. In the guided bend, a plunger or mandrel of defined dimensions forces the middle of the specimen between two supports set a fixed distance apart, or into a die: the bend geometry is imposed by the tooling, which makes the result reproducible, and that is why it is the method used in weld qualification. In the semi-guided bend, the specimen is bent in contact with the mandrel to the specified angle or inside radius, which is the typical case for plates, bars and rebar. In the free bend, the ends are brought together with no transverse force on the bend and nothing touching the inner face; it is usually used to complete a bend started by another method, up to 180°. In the bend and flatten test, after bending, a transverse force is applied until the legs touch along their full length, which is equivalent to bending over a mandrel of zero diameter.
Outside ASTM E290 there are other variants. In the wraparound bend, the specimen is clamped at one end and a roller rotates 180° around the mandrel, wrapping the specimen around it; it is used for low-elongation materials and aluminum welds. In the bend and rebend test for rebar, the bar is bent, artificially aged and bent back, which checks whether it is still ductile after aging. In the reverse (alternating) bend test, thin sheets and wires are bent repeatedly in opposite directions. The table summarizes the types and where each is used:
| Type | How it is done | Typical use |
|---|---|---|
| Guided (plunger and die) | a plunger of defined dimensions forces the middle of the specimen between two supports or into a die | weld qualification (face, root and side bends) |
| Wraparound (roller) | the specimen is clamped at one end and a roller rotates 180°, wrapping it around the mandrel | low-elongation materials, aluminum welds |
| Semi-guided | the specimen is bent in contact with the mandrel to the specified angle or radius | plates, bars, rebar |
| Free | the ends are brought together with no transverse force on the bend and no inner contact | completing a bend to 180° |
| Bend and flatten | bend followed by flattening between platens | thin sheets, wires |
| Bend and rebend | bend, artificial aging (100 °C for 1 h) and bend back | rebar (ISO 15630-1) |
| Reverse (alternating) | repeated bends in opposite directions | thin sheets and wires |
How much the outer face stretches: mandrel severity
The severity of the test is set by the ratio between the mandrel diameter (D) and the thickness or diameter of the specimen (t). In the bend, the outer face elongates and the inner face shortens; between them lies a layer that does not change length, the neutral axis. With the neutral axis at mid-thickness, the engineering strain in the outer fiber is:
ε = t / (D + t)
The smaller the mandrel relative to the thickness, the tighter the bend and the greater the strain the outer face must withstand. The chart below shows this curve, with the mandrel diameter expressed in thicknesses, and marks the mandrels required for CA-25, CA-50 and CA-60 rebar and the 4t mandrel of the welding standards.
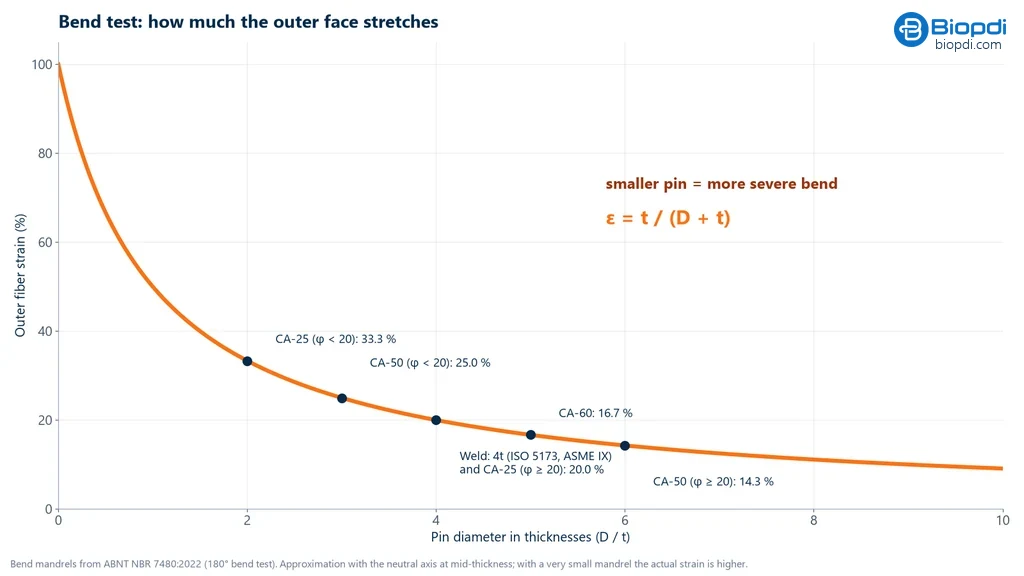
The table gives the values for the most common mandrels and where each one is used:
| D / t | Outer fiber strain | Where it is used |
|---|---|---|
| 0 (bent flat on itself) | 100% | bend and flatten, very ductile materials |
| 2 | 33.3% | CA-25 rebar with φ < 20 mm |
| 3 | 25.0% | CA-50 rebar with φ < 20 mm |
| 4 | 20.0% | welds with elongation ≥ 20% (ISO 5173, ASME IX); CA-25 with φ ≥ 20 mm |
| 5 | 16.7% | CA-60 rebar |
| 6 | 14.3% | CA-50 rebar with φ ≥ 20 mm |
The calculation explains the rule in the welding standards: the 4t mandrel imposes exactly 20% strain on the outer face, which is why it is used for materials with an elongation of at least 20%. For materials with lower elongation, ISO 5173 requires solving the same equation for the mandrel: d = 100·ts / A − ts, where ts is the specimen thickness and A is the minimum elongation of the material, in %. The formula is an approximation: with a very small mandrel, the neutral axis shifts inward and the actual strain is higher. The bend strain is also local, so it exceeds the minimum elongation from the tensile test, which is an average over the gauge length.
Bend test specimen
Under ISO 7438, the specimen may have a round, square, rectangular or polygonal cross section. Round bars up to 30 mm are tested at full cross section, as produced; so are rebar and wire. Plates yield rectangular specimens, and the thickness t is used to select the mandrel and the distance between supports. The length is not a fixed value: it depends on the thickness and the fixture, and must be enough for the legs to clear the supports and for the bend to reach the specified angle.
The main concern is the surface and the edges, because that is where cracks start. The zone affected by shearing or flame cutting, which is work hardened or hardened, is removed by machining. The edges are rounded: radius up to 1 mm for thickness below 10 mm, 1.5 mm from 10 to 50 mm and 3 mm above 50 mm. A sharp or burred edge opens an edge crack that has nothing to do with the material. For welded joints, specimen extraction and preparation have their own rules, described in the weld section.
How to perform the bend test (ISO 7438)
- Prepare the specimen as described above: free of the cut-affected zone and with rounded edges.
- Select the mandrel according to the product standard (NBR 7480, welding code, plate specification).
- Set the distance between supports: l = (D + 3a) ± a/2, where a is the thickness. Supports that are too close, with l ≤ D + 2a, trap the specimen and cause stretching instead of bending.
- Bend to the specified angle, between 10 °C and 35 °C, without reversing the direction of loading. For rebar, use freely rotating supports.
- Examine the convex face with the unaided eye, or with a magnifier if the standard requires it, and measure the discontinuities. Under ASTM E290, cracks within one thickness of the edge are not counted.
- Report the standard, mandrel, angle, position and size of the discontinuities, and the result.
ABNT NBR 6153 (the former Brazilian bend test standard), which many texts still cite, was withdrawn in 2015 and replaced by ABNT NBR ISO 7438.
Rebar bend test (NBR 7480)
ABNT NBR 7480:2024 (the Brazilian standard for steel bars and wires for reinforced concrete) requires bars and wires for reinforced concrete to be bent to 180° over the mandrel in the table below without fracture or cracking in the tension zone. The mandrel is given as a multiple of the nominal bar diameter, φ. The test method is that of ABNT NBR 17005:2021.
NBR 17005 is short and practical. It accepts two arrangements: two supports and a mandrel, which is the fixture mounted on a universal testing machine, or a fixed support, a bending mandrel and a movable support that guides the bar around the mandrel, as in a bar bender. In the two-support arrangement, these are the points that most affect the result:
- Distance between supports: l = (D + 3a) ± a/2, with D the mandrel diameter and a the bar size. For 12.5 mm CA-50 and a 3φ mandrel (37.5 mm), l = 75 ± 6 mm. The distance must not change during the test, and the minimum exists so the bar does not jam between the supports and get stretched instead of bent.
- Rotating supports: the supports must rotate freely, and the supports and mandrel must be longer than the bar diameter and have a rounded, hard surface so as not to mark the bar.
- No pause: once started, bending stops only when the two legs of the specimen are parallel, at 180°.
- Specimen from the bar as supplied: not machined; coiled wire is straightened carefully, and drag or cutting marks that are not representative of the lot invalidate the specimen.
- Examination and report: the outer face of the bend is examined with the unaided or corrected eye for fracture, cracks or fissures. The report gives the standard, manufacturer, grade, bar size, heat or lot, equipment and result.
A reading caveat: the 2021 text of NBR 17005 refers to the mandrel table of NBR 7480:2007. The table of the current edition of NBR 7480 applies, reproduced below in values.
| Grade | Mandrel (φ < 20 mm) | Mandrel (φ ≥ 20 mm) | Minimum elongation over 10φ |
|---|---|---|---|
| CA-25 | 2φ | 4φ | 18% |
| CA-50 | 3φ | 6φ | 8% |
| CA-60 | 5φ | not applicable | 5% |
The test mandrel is not the job-site mandrel: NBR 6118 (the Brazilian standard for the design of concrete structures) requires bars to be bent on site over larger mandrels (CA-50: 5φ for φ < 20 mm and 8φ for φ ≥ 20 mm), meaning that site bending is less severe than the release test. The tensile requirements for rebar are covered in ductility.
Weld bend test
In welding procedure and welder qualification, specimens taken transverse to the weld are bent to 180° with the weld metal and the heat-affected zone fully within the bent portion. The weld reinforcement is removed first so it does not create a stress concentration. There are three variants, depending on which side of the weld is placed in tension. They are covered in detail, along with the transverse tensile test and the procedure on the universal testing machine, in the article on the weld test specimen:
- Face bend: the weld face is in tension.
- Root bend: the root is in tension. This reveals lack of penetration.
- Side bend: the cross section is in tension. It is used on thick plates (10 mm and over in ASME IX).
Under ASME IX, procedure qualification on plate under 19 mm requires 2 face bend and 2 root bend specimens, and above that thickness 4 side bend specimens. Welder qualification requires 1 face bend and 1 root bend. The typical jig for ordinary steel uses a 10 mm (3/8") specimen and a 38 mm (1-1/2") plunger, which is the 4t mandrel.
What is measured in a weld bend test
You measure the size, in millimeters, of the open discontinuities on the convex surface and compare it with the code limit, you check the angle reached, and, when required, you measure the bend elongation over a gauge length. The table compares the limits of the three most widely used codes:
| Criterion | ASME IX (QW-163) | AWS D1.1:2025 | ISO 5173:2023 |
|---|---|---|---|
| Individual discontinuity | 3 mm maximum | 3 mm maximum | set by the application standard |
| Sum of discontinuities | not applicable | up to 10 mm (indications from 1 to 3 mm) | same as above |
| Corner crack | not counted unless it comes from an internal defect | up to 6 mm, unless it originates from slag or lack of fusion | same as above |
| Angle | 180° | 180° | about 180° |
ISO 5173 describes the test but gives no acceptance criteria. Those come from the qualification standard (ISO 15614-1 for procedures and ISO 9606-1 for welders).
Solved bend test examples
1. Severity of a mandrel. A 10 mm plate bent to 180° over a 40 mm mandrel: ε = 10 / (40 + 10) = 20%. This is the 4t condition of ASME IX and ISO 5173.
2. CA-50 rebar (a Brazilian rebar grade). 16 mm bar: mandrel of 3φ = 48 mm and ε = 16 / 64 = 25%. 25 mm bar: mandrel of 6φ = 150 mm and ε = 25 / 175 = 14.3%. The thicker bar gets a proportionally larger mandrel.
3. Mandrel and rollers per ISO 5173. A 10 mm face bend specimen, with base metal having a minimum elongation of 16%: d = 100 × 10 / 16 − 10 = 52.5 mm (check: 10 / 62.5 = 16%). ISO 5173 sets the distance between rollers between d + 2ts + 1 and d + 3.5ts, that is, between 73.5 mm and 87.5 mm.
4. Supports per ISO 7438. An 8 mm bar over a 24 mm mandrel: l = (24 + 24) ± 4 = 48 ± 4 mm. At 40 mm or less, the bar would bind and the test would be invalid.
5. Weld acceptance. After 180°, the convex surface shows indications of 2.0, 2.5, 0.8 and 1.5 mm and a 5 mm corner crack with no sign of slag. Under AWS D1.1: largest indication 2.5 mm (limit 3 mm), sum of indications between 1 and 3 mm 6.0 mm (limit 10 mm) and corner crack 5 mm (limit 6 mm): accepted. Under ASME IX as well. If the corner crack showed slag, the limit would drop to 3 mm and the specimen would be rejected.
Bend testing of sheet, tubes and other materials
On metal sheet, the bend test checks whether the sheet can withstand the forming it will undergo in fabrication: the sheet specification defines the mandrel and the angle, and the bend is performed on specimens taken from the sheet, with the sampling direction recorded, because rolled sheet can crack in one direction and not in the other. On tubes, the full-section tube bend test (ISO 8491) and the ring flattening test (ISO 8492) are used. They assess the ductility of the tube and, in welded tubes, of the weld seam.
For polymers, ceramics and composites, the test done in practice is not bending to an angle with inspection for cracks, but the flexural test, which records the force × deflection curve and calculates the flexural strength and flexural modulus in MPa. For plastics, the standards are ISO 178 and ASTM D790. Ceramics, too brittle to bend, are tested in 3-point or 4-point flexure to fracture. A "bend strength" value in MPa is therefore the result of a flexural test.
Common mistakes in bend testing
- Citing NBR 6153 (a former Brazilian bend test standard) as current. It was withdrawn in 2015.
- Treating a bend test as a flexural test. The bend test assesses plastic deformation and cracking, not strength.
- Using the on-site bending mandrel (NBR 6118, the Brazilian concrete structures design code) in the acceptance test (NBR 7480, the Brazilian standard for steel reinforcing bars), or the other way around, or using the old NBR 7480 table.
- Sharp or burred edges, which cause false edge cracks.
- Supports too close together, which bind the specimen and cause stretching.
- Fixed supports on rebar, which lock the bar; use freely rotating supports.
- Not removing the weld reinforcement, or machining the specimen to hide a defect.
- Wrong mandrel for low-elongation material, such as high-strength steel or welded aluminum.
- Citing EN 10045 as a bend test standard: it covered Charpy impact testing and was withdrawn, replaced by ISO 148-1.
Bend test standards
The standard to follow depends on what is being tested: ISO 7438 and ASTM E290 give the general method for metals, while rebar and welds have their own standards that set the mandrel and the acceptance criteria. The table lists the most widely used ones:
| Standard | Application | Edition |
|---|---|---|
| ABNT NBR ISO 7438 / ISO 7438 | bend testing of metallic materials | ISO 7438:2020; ABNT NBR ISO 7438:2022 (Brazilian adoption) |
| ASTM E290 | bend testing for ductility | E290-22 |
| ASTM E190 | guided bend testing of welds | E190-21 |
| ABNT NBR 7480 | rebar (Brazil): requirements, bending mandrels | 2024 (equivalent to the 2022 edition corrected by Amendment 1) |
| ABNT NBR 17005 | bend test method for bars and wires for reinforced concrete (Brazil) | 2021 |
| ISO 15630-1 | bend and rebend testing of rebar | 2019 |
| ISO 5173 | bend testing of welds | 2023 |
| ASME BPVC Section IX | welding qualification (QW-160 to QW-163) | |
| AWS D1.1 | structural welding of steel | 2025 |
| ISO 8491 and ISO 8492 | bend and flattening tests of tubes | 1998 and 2013 |
| ABNT NBR 6153 | semi-guided bend test (Brazil) | withdrawn in 2015 |
Bend testing machine
On the universal testing machine (UTM), the bend fixture (two supports, preferably freely rotating rollers, and a former or plunger) replaces the grips. The load cell records the force and the displacement of the former, and the angle can be calculated from that displacement. The Biopdi line of universal testing machines performs bend tests, including with a fixture conforming to ISO 5173, and the capacity depends on the thickness and the bar diameter: 10 mm weld specimens and small-diameter rebar fit in the 5 to 50 kN range, while large-diameter rebar calls for the 200 kN or 300 kN models. The same machine performs the tensile test on the bars, which completes the acceptance of the lot. The panel below shows the machine, the role of each part in the bend test and the fixture used.
The universal testing machine in the bend test
The M2 line has single-column models, from 200 N to 10 kN, and dual-column models, from 5 kN to 1,000 kN. Each part of the machine has a role in the test:
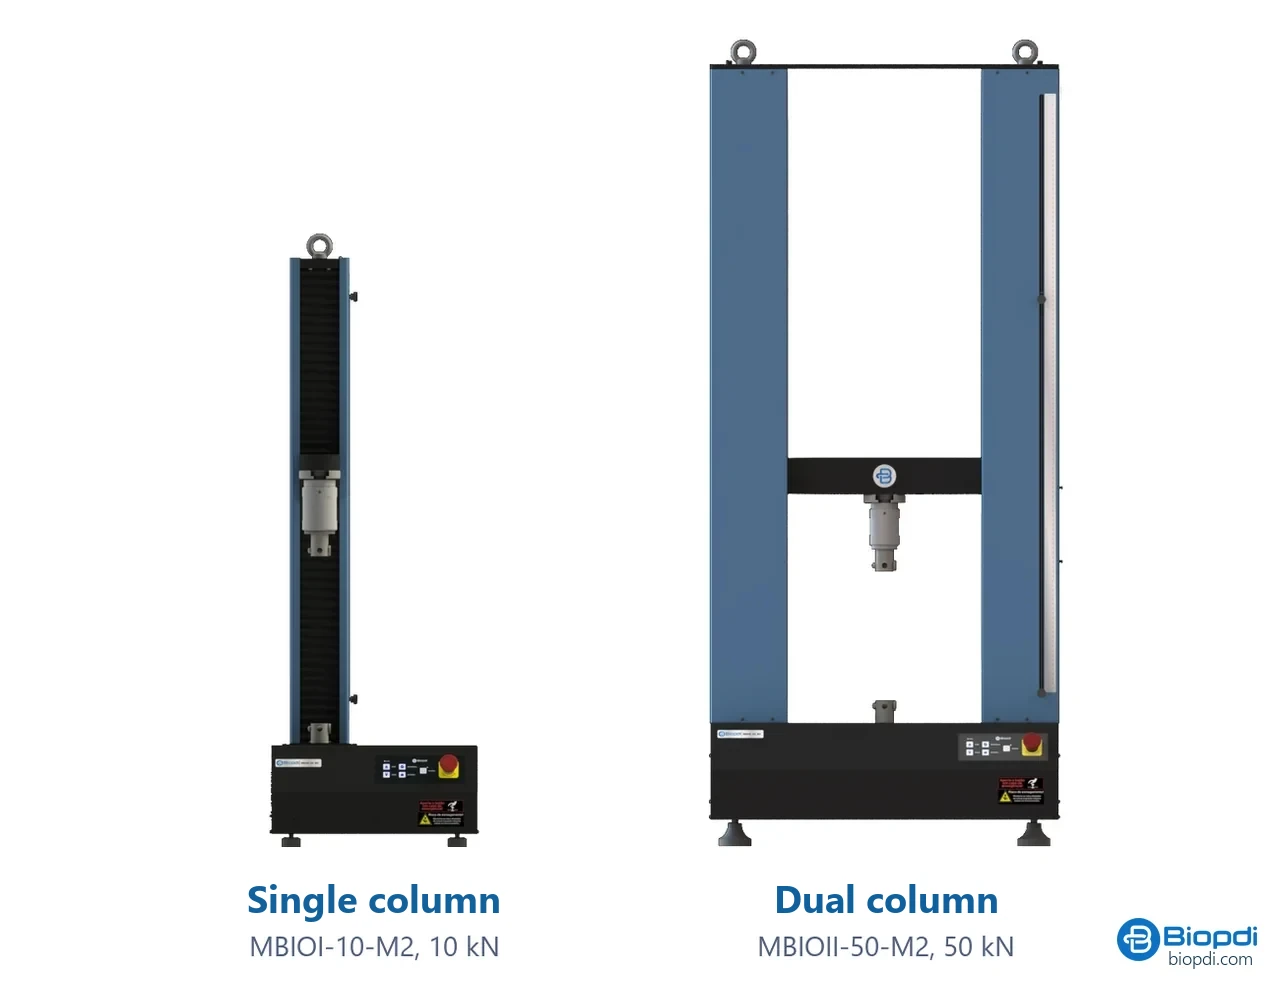
- Moving crosshead lowers the former between the supports
- Load cell records the bending force
- Bend fixture rollers and formers of 2t, 4t, 6t...
- Angle calculated from the former displacement
- BioLab software force × displacement up to 90° or 180°
- Control panel and emergency stop positions and stops the test
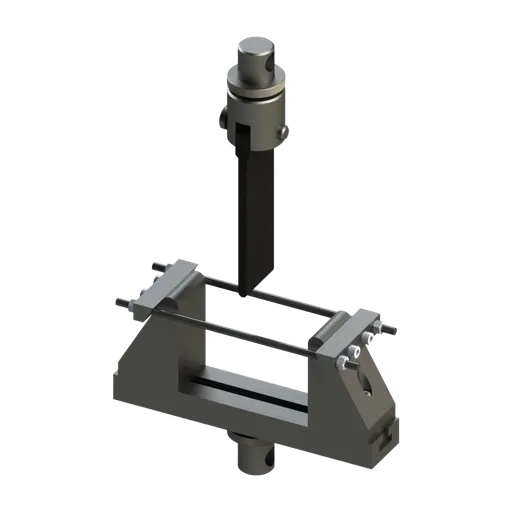
Bend test fixtures
The fixtures below are mounted on the same machine, depending on the specimen and the standard:
Other tests and technical references
Tests performed on the Biopdi universal testing machine
Related technical references
Test specimen: what it is, types by test and material, standards and dimensions
A test specimen is a sample whose shape and dimensions are set by the test standard. See types, standards and sizes for metal, plastic, concrete, wood and welds.
Materials testing: what it is, types, destructive and non-destructive testing, standards and how to choose
Materials testing is the standardized procedure that measures the mechanical, physical, chemical or microstructural properties of a representative sample, or that inspects a part without damaging it. See the five families of tests, the difference between destructive and non-destructive testing, the test specimen, accreditation, the standards and how to choose the right test.
Mechanical testing: what it is, types, what each test measures and standards
Mechanical tests apply a controlled load to a test specimen and measure the material's response. See the types (destructive, non-destructive, static and dynamic), what each test measures, the standards and the machine for each one.
Frequently asked questions
What is a bend test?
It is a qualitative test in which a specimen is bent over a mandrel of defined diameter to 90° or 180° and checked for cracks on the tension side. It assesses the ductility and soundness of the material, mainly of welds and rebar.
What is the bending process?
In metal forming, it is the plastic deformation of a sheet or bar around an axis: the outer surface is in tension and the inner surface in compression. The bend test uses the same mechanism to check whether the material can withstand this deformation without cracking.
What are the types of bend test?
Under ASTM E290: guided, semi-guided, free, and bend and flatten. In practice, the wrap-around bend (with a roller), the bend and rebend test of rebar and the reverse bend test of thin sheet and wire are also used.
What is the mandrel diameter for CA-50 rebar?
Under ABNT NBR 7480:2024 (the Brazilian rebar standard), 3φ for bars under 20 mm and 6φ for bars of 20 mm or more, bent to 180° without fracture or cracking. For CA-25 it is 2φ and 4φ, and for CA-60, 5φ.
What is measured in the bend test of welded specimens?
The size, in millimeters, of the open discontinuities on the convex surface, compared with the code limit (3 mm in ASME IX and AWS D1.1), and the angle reached. Bend elongation is sometimes measured as well.
What is the ASME IX bend test acceptance criterion?
No open discontinuity larger than 3 mm in any direction on the convex surface, with the weld and heat-affected zone fully within the bent portion. Corner cracks are not counted unless they come from an internal defect.
What is the difference between face, root and side bends?
In a face bend, the weld face is in tension; in a root bend, the root; in a side bend, the weld cross section, used on thick plates.
Is NBR 6153 still in force?
No. ABNT NBR 6153 was withdrawn in 2015 and replaced by ABNT NBR ISO 7438.
What is the difference between a bend test and a flexural test?
The flexural test is quantitative: it measures strength in MPa and the flexural modulus. The bend test is qualitative: the specimen is bent to an angle and checked for cracks.
Why is a smaller mandrel more severe?
Because the strain on the outer surface is ε = t / (D + t): the smaller the mandrel diameter relative to the thickness, the more the outer surface stretches. A 2t mandrel imposes about 33%; a 6t mandrel, about 14%.
What machine performs the bend test?
A universal testing machine with a bend fixture, a press with a fixture, or a rebar bending machine with freely rotating supports. The universal testing machine records force and displacement and also performs the tensile test on the same material.